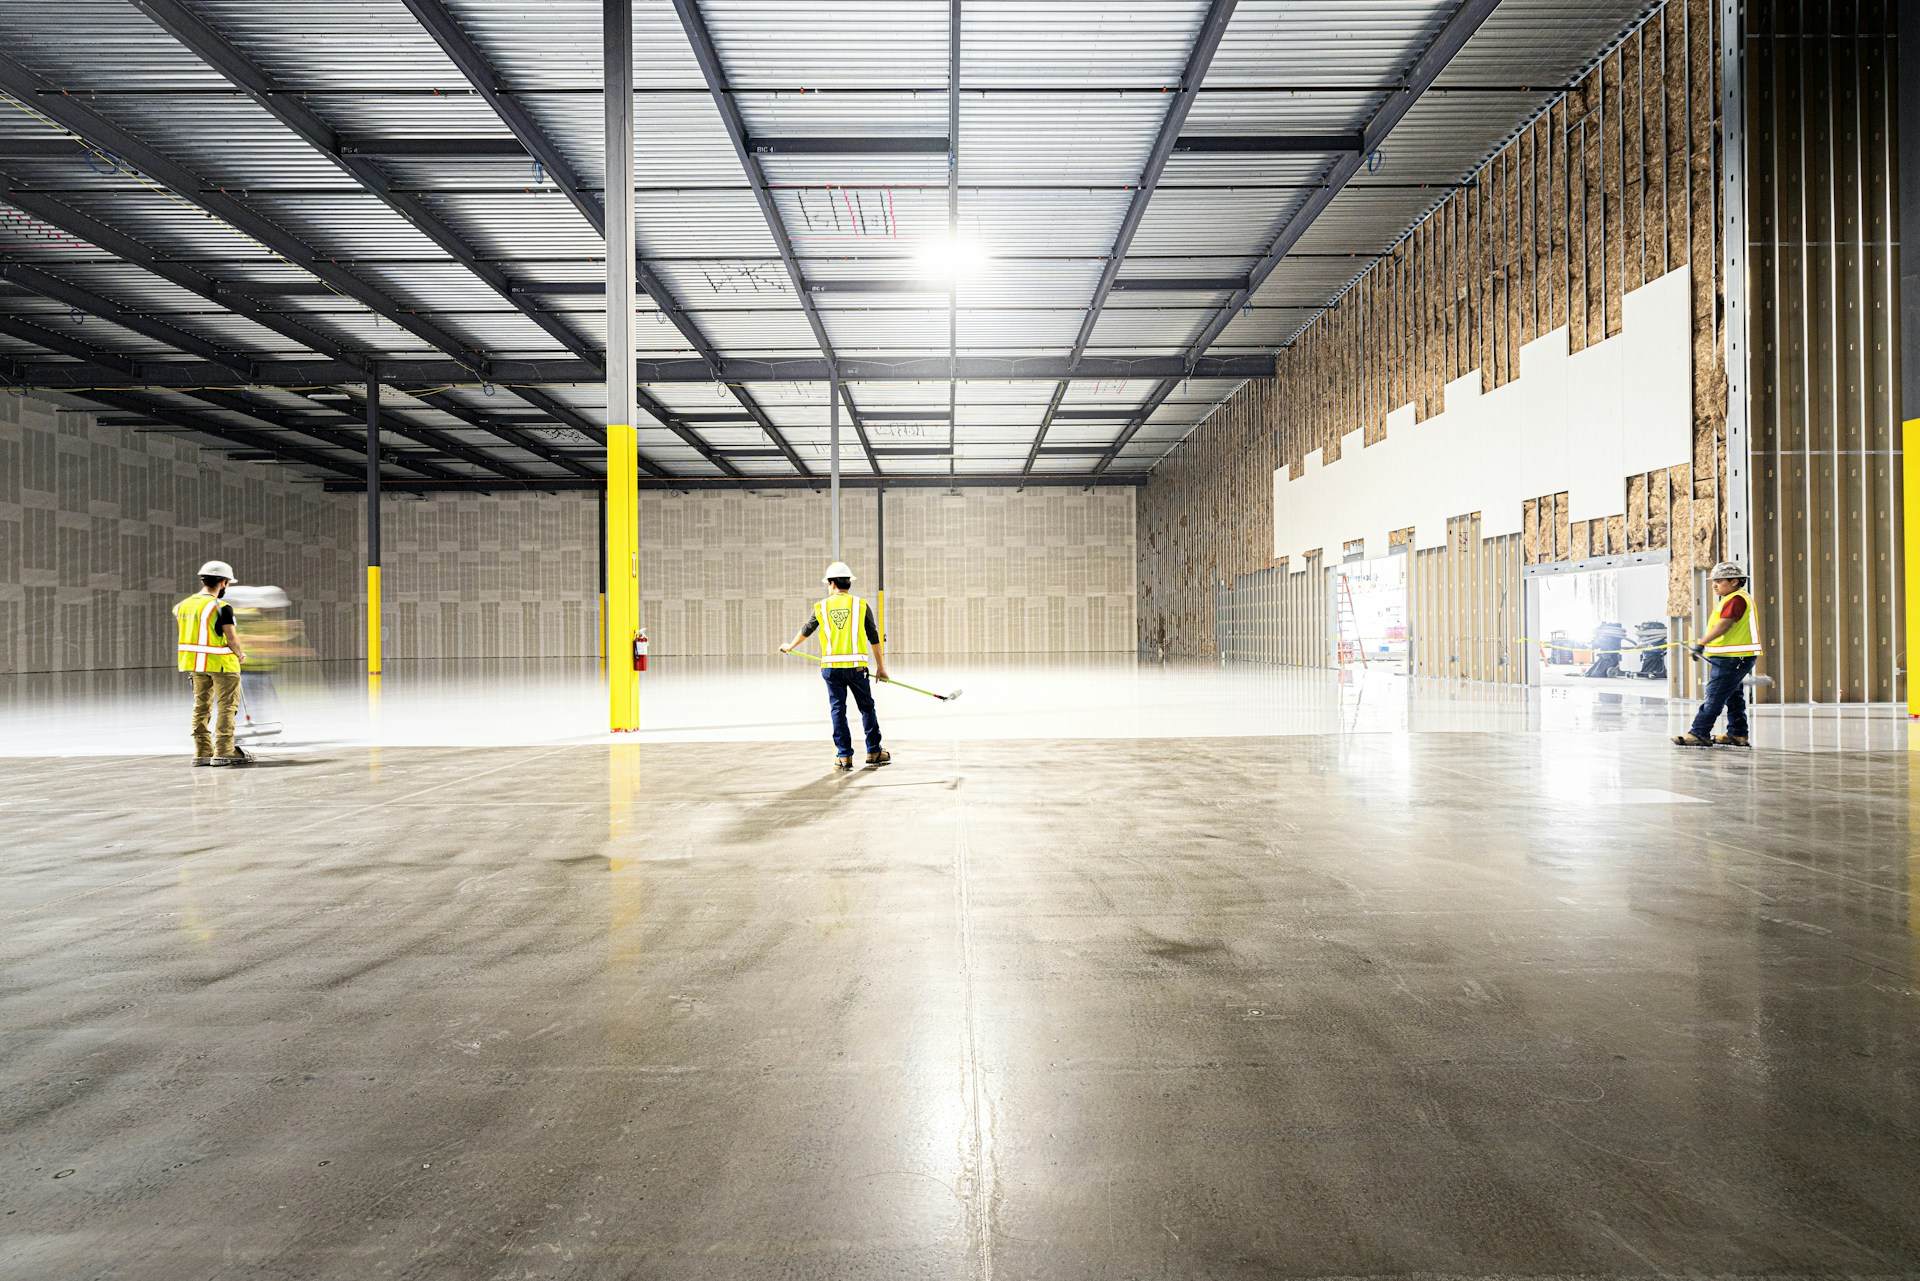
Factory floor downtime becomes more expensive as a growing manufacturer adds orders, equipment, and employees. One stopped process can leave operators waiting, delay downstream work, and push a full production schedule into overtime.
Avoiding every interruption is unrealistic, but scaling makers can reduce both the frequency and duration of shutdowns. The work starts with understanding which assets can stop production, then building simple maintenance routines around them. Those routines should cover production equipment, support systems, operator checks, and replacement parts. Documented procedures also help newer employees respond consistently as the business expands.
Map Your Single Points of Failure
Create a process map that follows each product from incoming material through packing and shipment. At every stage, identify the equipment, software, utility, and employee knowledge required to keep work moving. A single point of failure is any resource whose loss would stop the process because no ready substitute exists. This practical guide to single point identification explains the underlying concept and ways to reduce exposure.
Rank each failure point according to its likely effect. Consider how many production hours it could interrupt, how long recovery would take, and how many orders could be delayed. A specialized machine with a six-week component lead time deserves more attention than a common workbench tool that can be replaced locally in a few hours.
Your map should include less obvious dependencies. One experienced technician may be the only person who knows how to reset a controller or calibrate a machine after maintenance. A single network switch could connect several production stations. One air compressor may supply every pneumatic process in the building. Business continuity planning can help you examine these operational dependencies beyond the main production line.
Assign an owner and a backup plan to every high-risk item. Possible controls include cross-training employees, arranging access to rental equipment, or setting up an alternate workflow. Review the map after equipment purchases, layout changes, and major hiring periods because growth regularly creates new dependencies.
Maintain Crucial Support Systems
Support equipment often receives less attention than the machines producing saleable goods, yet its failure can stop several work areas at once. Air compressors, ventilation equipment, electrical panels, network hardware, and material handling systems all need documented maintenance schedules. Include cleaning, inspection, lubrication, calibration, and filter replacement intervals based on operating conditions and manufacturer guidance.
Dust collection and air filtration systems require particular attention because restricted airflow can affect equipment performance and working conditions. Facilities that already run compatible systems can source genuine or compatible replacement filters and parts for a Torit dust collector before a worn component causes an unplanned shutdown. Record pressure readings and other condition indicators at consistent intervals so your maintenance team can detect gradual changes.
Tie maintenance frequency to actual use. Equipment running two shifts each day may need service based on operating hours, while seasonal machinery may be better served by pre-start and post-season checks. A calendar-only schedule can miss heavy production periods when components accumulate wear faster.
Support systems tied to connected controls also need digital oversight. The publisher’s guide to essential network monitoring strategies explains how alerts, device visibility, and escalation procedures can prevent a minor network issue from becoming prolonged downtime.
Keep completed maintenance records in one shared location. Those records should show the task, date, readings, parts used, and person responsible. Consistent data lets you spot recurring faults and adjust service intervals before problems spread across the floor.
Standardize Daily Operator Inspections
Operators see equipment behavior every day, which puts them in a strong position to catch early signs of trouble. Give each workstation a short inspection checklist that can be completed at startup, during a shift change, or at shutdown. Five focused checks completed consistently provide more value than a long form that employees rush through.
Tailor each checklist to the equipment. An operator might confirm that guards and sensors are in their expected condition, inspect for loose fittings, listen for unusual sounds, and note temperature or pressure readings. The form should also include a clear place to record leaks, vibration, slow cycle times, and error messages. Avoid vague prompts such as “check machine” because different employees will interpret them differently.
Set limits that trigger action. For example, a reading inside the normal range can be recorded and monitored, while a reading outside the defined limit should create a maintenance request. Operators also need to know when they should stop a process and contact a supervisor. Established machine downtime reduction practices emphasize planned maintenance, accurate production data, and early reporting instead of waiting for equipment to fail completely.
Train employees with examples taken from your own floor. Show them what normal operation sounds like, where approved readings appear, and how to report a concern. Include inspection training in onboarding and verify competency after several supervised shifts.
Supervisors should review completed forms promptly. If operators report problems but see no response, participation will decline. Closing the loop with a note about the repair or monitoring plan shows that each inspection has a practical purpose.
Keep Critical Spare Parts on Hand
Build a critical spares list from your failure map, maintenance records, and equipment manuals. Focus on parts that fail often, have long supplier lead times, or can stop an entire production stage. Common candidates include sensors, belts, bearings, filters, relays, fuses, and control components, though the correct inventory will depend on your specific machines.
Calculate the cost of carrying each part against the cost of waiting for it. A $600 component may appear expensive to keep on a shelf, but the decision changes if its failure stops a line that produces $5,000 of finished work per shift. Use realistic supplier lead times, including possible shipping delays and the time needed for installation.
Organize spares by equipment and assign each item a stock number, storage location, and minimum quantity. Label shelves clearly and protect sensitive components from moisture, dust, or temperature extremes. Someone should record every withdrawal immediately. Otherwise, the inventory system may show a part that no longer exists.
Review shelf life and compatibility during scheduled stock checks. Filters, seals, lubricants, and electronic components may degrade in storage or become obsolete after an equipment upgrade. Rotate dated items where possible and confirm that replacement parts match current machine configurations. Broader failure prevention strategies can also help teams decide where redundancy or backup capacity deserves investment.
Finally, establish supplier contacts before an emergency. Record normal lead times, after-hours details, and approved alternatives. A short list of verified sources saves valuable time when your on-hand stock has already been used.
Downtime control improves when these practices become part of normal production management. Review the failure map during expansion planning, examine inspection reports at daily meetings, and update spare-part levels when demand changes. The most useful result is a factory floor where a warning sign leads to a defined response before the production schedule starts to slip.